
High Volume Metal Stamping: How to Scale Production from Prototype to Mass Production for Custom Metal Stamping Parts
Direct answer: High volume metal stamping becomes cost-effective above 50,000 pieces per year, where progressive die tooling cost is amortized over enough units to drop per-piece cost by 40 to 70 percent compared to soft tooling. VOLCRIX runs serial production up to 1,000,000 pieces per month on progressive dies for automotive, EV, and industrial customers. The path from prototype to high-volume production runs through three gates: DFM validation, soft tool bridge production, and hard tool PPAP qualification.
Common Applications
- Automotive wire harness terminals — brass C26000 and phosphor bronze C51000 terminals running 1 to 5 million pieces per month for Tier 1 harness manufacturers.
- EV battery cell contacts and busbars — copper C11000 and aluminum 6061-T6 progressive die stampings at 200,000 to 1,000,000 pieces per month for battery pack assembly.
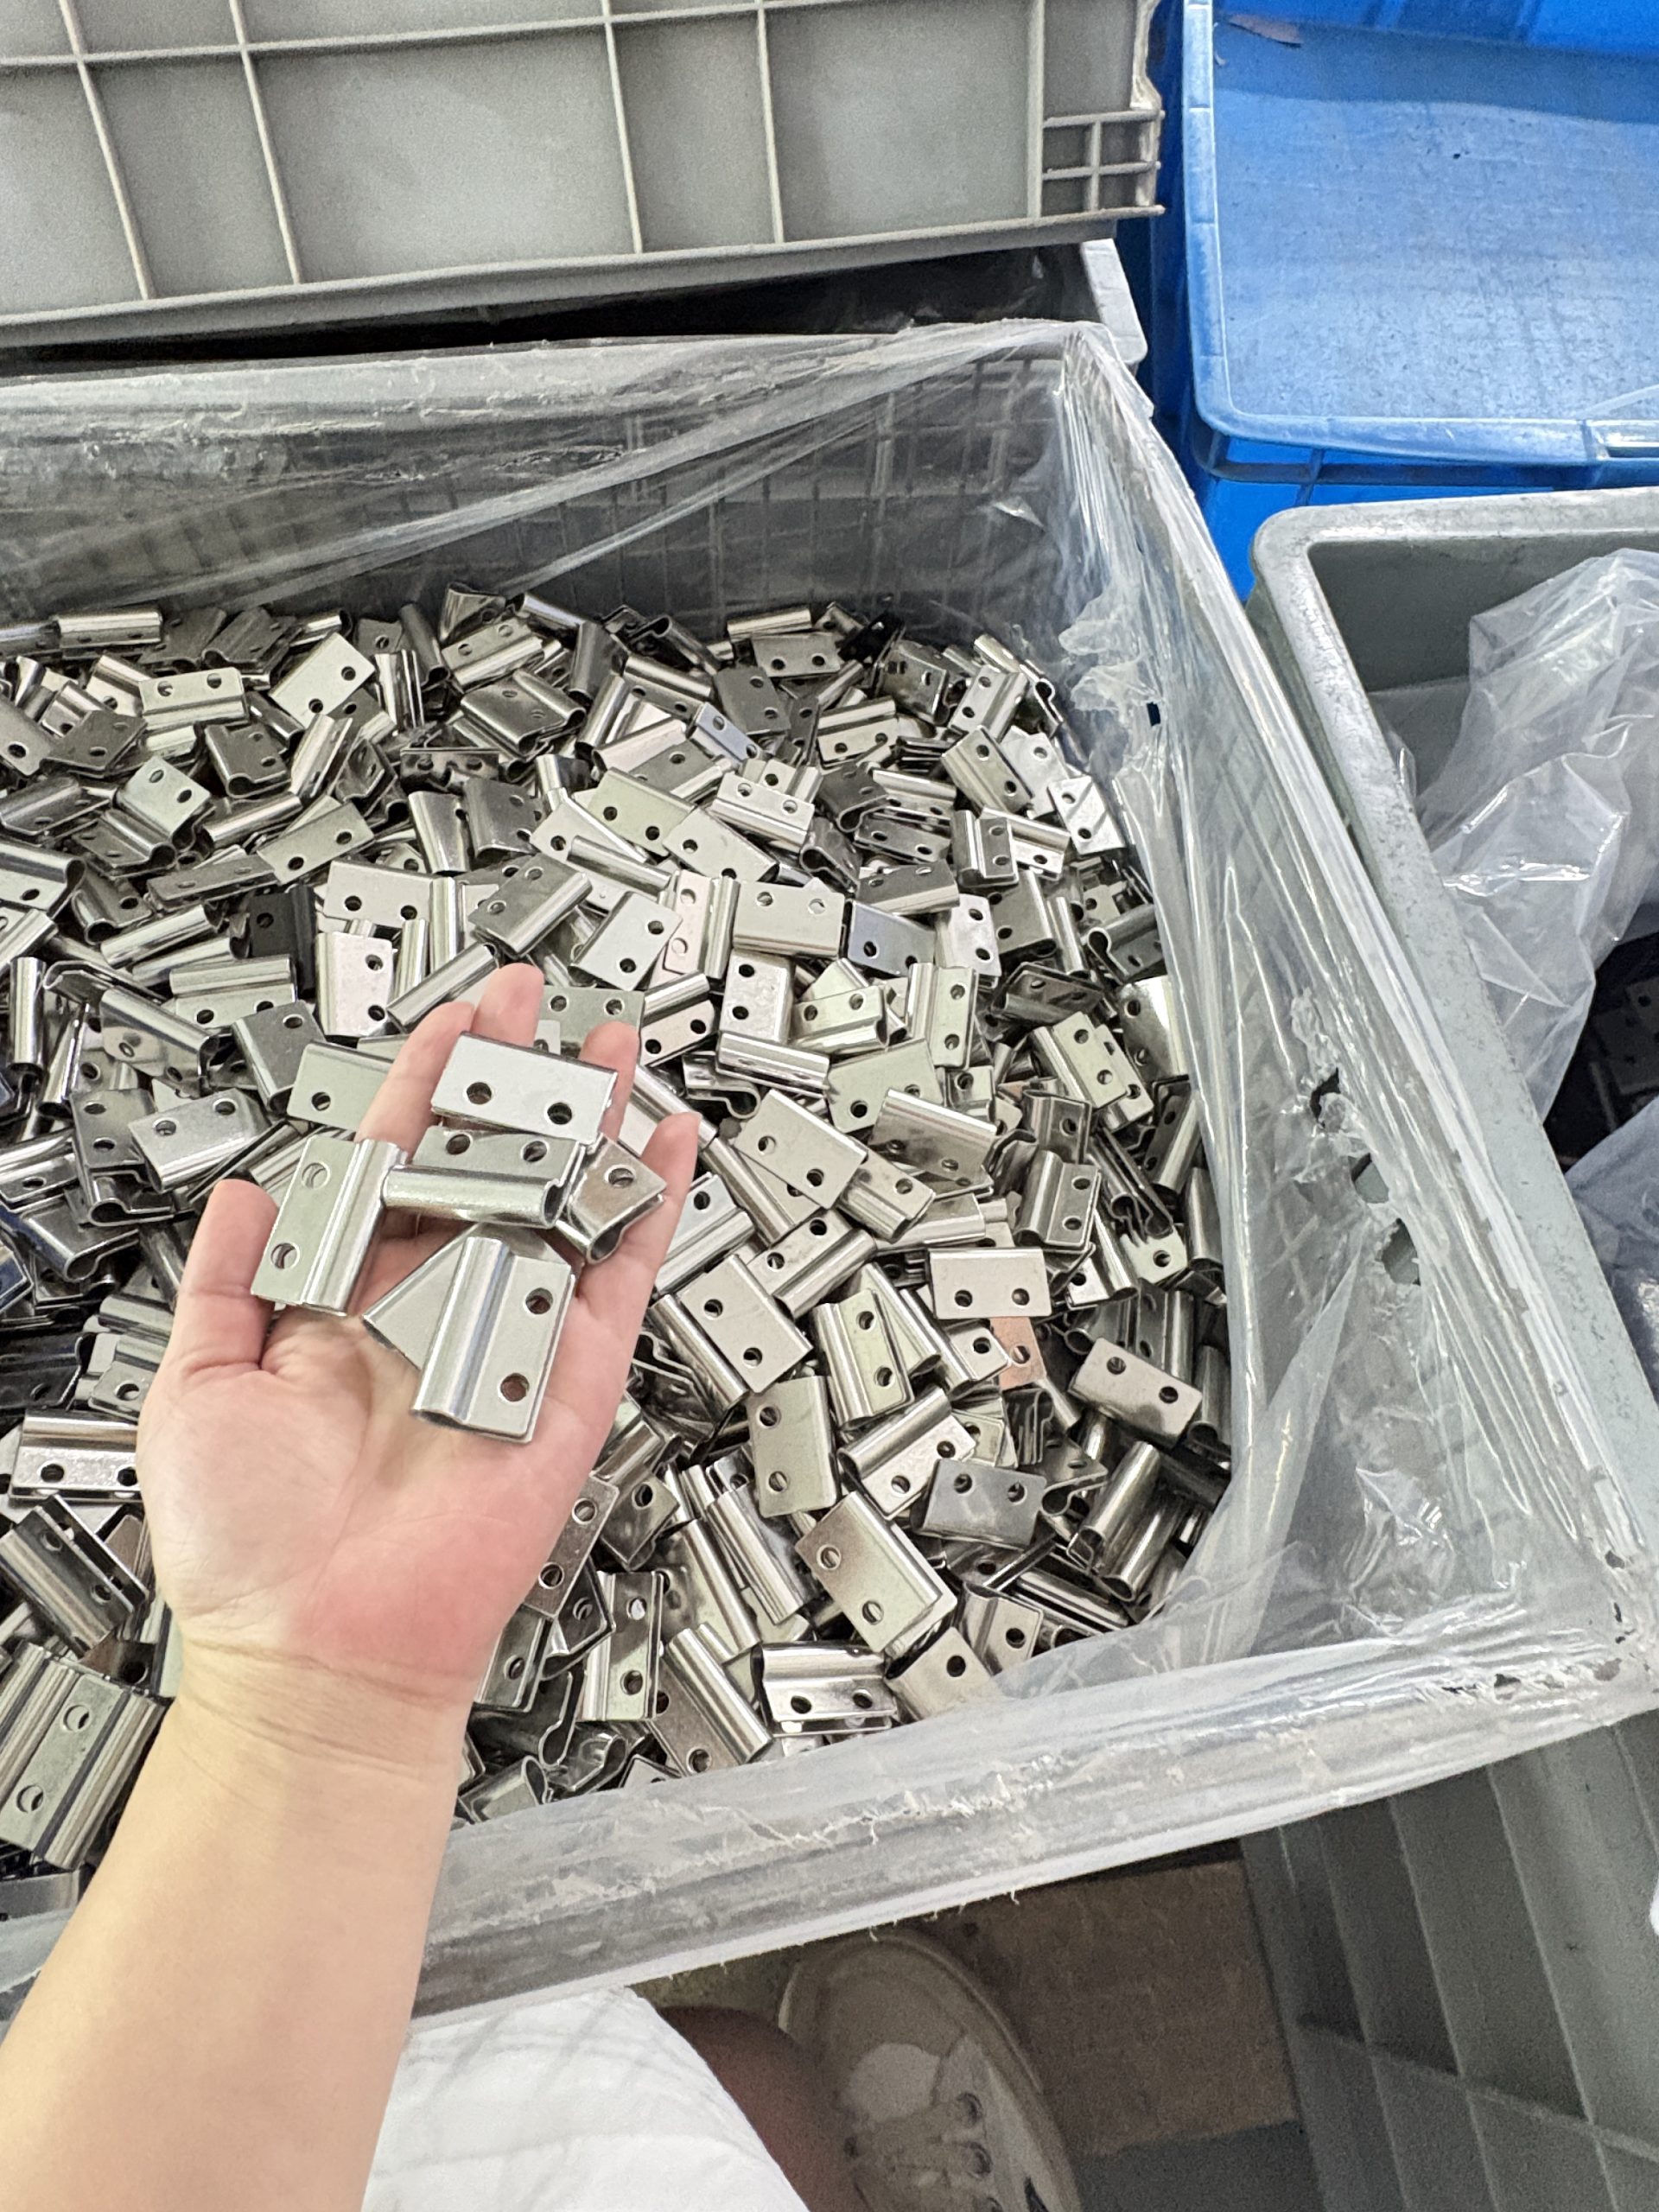
- Industrial brackets and mounting hardware — cold-rolled steel and galvanized steel stampings at 100,000 to 500,000 pieces per month for HVAC and switchgear OEMs.
- Spring contacts and EMI shielding — beryllium copper C17200 and 301 stainless stampings at 50,000 to 300,000 pieces per month for consumer electronics and telecom.
Manufacturing Support from VOLCRIX
- Capacity planning with you. we model annual volume, lot sizes, and release patterns to size the right number of presses, dies, and operators for your program.
- Redundant press capacity. 40 mechanical and servo presses from 25 to 200 tons mean we can shift production between presses if a die is in maintenance.
- In-house die maintenance. our tool room handles die repair, punch replacement, and resharpening on the same campus as production, with 24 to 48 hour turnaround.
- Material stocking programs. for high-volume customers, we maintain 3 to 6 months of coil stock inventory with mill certificates to insulate against supply disruptions.
- IATF 16949 PPAP qualification. automotive programs go through PPAP Level 1 to Level 5 with full capability studies, control plans, and IMDS submissions.
The Prototype to High-Volume Stamping Path
Moving from a working prototype to high-volume production is the most critical phase of any stamping program. Done right, it is invisible to the buyer — parts arrive on time at the right cost. Done poorly, it costs weeks of delay and tens of thousands of dollars in scrap. Here is how we manage the transition at VOLCRIX:
- Gate 1: DFM validation. Before any tool is cut, our engineers review the drawing against your annual volume target, material availability, and tolerance requirements. We produce a written DFM report covering bend radii, grain direction, draw ratios, and tolerance feasibility.
- Gate 2: Soft tool bridge production. While the hard progressive die is being built (25 to 35 days), we produce 1,000 to 5,000 parts on soft tooling for design validation, customer samples, and pre-production builds. Soft tooling covers the gap between prototype and serial production.
- Gate 3: Hard tool tryout and first article. The progressive die is mounted on the production press, aligned, and run through controlled tryout. First article parts are inspected on a Zeiss CMM with full dimensional report.
- Gate 4: PPAP qualification. For automotive programs, we run capability studies (50 to 125 pieces), submit PPAP Level 3 documentation, and get customer sign-off before serial production.
- Gate 5: Serial production ramp. Production volume scales up over 4 to 8 weeks as operators learn the part, inspection routines stabilize, and packaging lines are validated.
Material Sourcing for High-Volume Programs
High-volume stamping programs require material sourcing that goes beyond one-off orders. We build supply continuity, cost stability, and quality consistency into our material programs. Here is how we approach it:
- Certified mill relationships. We source from Baosteel, POSCO, Acerinox, and other certified mills with whom we have multi-year relationships. Each shipment arrives with EN 10204 3.1 mill certificates.
- Slitted coil stock. For programs above 100,000 pieces per month, we slit coil stock to die-required width on our own slitter, reducing material cost and lead time.
- Safety stock programs. For Tier 1 automotive customers, we maintain 3 to 6 months of coil stock in our warehouse to insulate against mill disruptions.
- Pre-plated stock. For high-volume programs that require tin or nickel plating, we source pre-plated coil to eliminate the plating step and reduce per-piece cost.
- Multi-source qualification. For critical programs, we qualify two or more mills for each material grade, giving us flexibility if a mill has a supply disruption.
Tolerance Stability Over Die Life
Die wear is the primary cause of tolerance drift during high-volume production. Managing die wear is the difference between a stamping line that runs consistently for 500,000 strokes and one that drifts out of spec after 100,000 strokes. Here is our approach:
- Punch material selection. We use D2, A2, or carbide punches depending on the material being stamped and the expected die life. Carbide punches deliver 5 to 10 times the life of D2 punches on stainless steel and high-volume runs.
- Die surface treatments. Nitriding, CVD, and PVD coatings extend die life by reducing wear and galling. We select coating based on material and production volume.
- Punch re-sharpening schedule. Punches are re-sharpened at scheduled intervals based on stroke count and material. We keep spare punches for high-volume dies to avoid production stoppage during sharpening.
- Stripper and guide maintenance. Strippers, guides, and pilots are inspected and adjusted every 50,000 strokes. Worn strippers cause burrs and tolerance drift.
- In-process measurement. Keyence vision systems check critical dimensions every 30 strokes and alert operators to drift before parts go out of spec.
Production Planning and Release Management
High-volume stamping programs run on disciplined release patterns, kanban systems, or schedule-based releases. Here is how we manage production flow:
- Forecast-based capacity planning. We review your 12-month rolling forecast quarterly and right-size press capacity, die inventory, and staffing.
- Kanban release patterns. For many customers, we run kanban releases with safety stock at our factory. You call off against the kanban and we replenish within 5 to 10 days.
- Schedule-based releases. For larger lots (above 50,000 pieces), we run schedule-based releases with weekly or bi-weekly shipments against your production schedule.
- Safety stock levels. Standard safety stock is 2 to 4 weeks of demand. For critical automotive programs, we maintain higher safety stock levels per contractual requirements.
- Expedited response. When demand spikes, we have redundant press capacity that can be brought online within 24 to 48 hours for most part types.
Buyer Checklist Before You Issue the RFQ
- Share your 3 to 5 year volume forecast — die material, surface treatment, and number of stations depend on total program volume, not just first-year quantity.
- Define lot size and release pattern — weekly kanban releases of 5,000 pieces drive different die and staffing decisions than monthly releases of 50,000 pieces.
- Identify supply continuity requirements — for Tier 1 automotive programs, dual sourcing, safety stock, and tooling backup plans are often contractually required.
- Specify packaging and labeling requirements — high-volume production requires bulk packaging, bar-coded labels, and often customer-specific dunnage; specifying these upfront avoids repack charges.
- Plan for design changes early — engineering change orders on a high-volume die can cost weeks of downtime; designing flexibility into the die pays off across the program life.
Related Custom Manufacturing Services
Custom Metal Stamping Parts | Custom Progressive Die Stamping | EV Battery Busbar Stamping | Automotive Metal Stamping Parts
Why VOLCRIX for This Program
Since 1991, VOLCRIX has run a single factory in Yueqing, Wenzhou, focused on precision metal forming and machining for export B2B programs. The reason buyers come back: every step happens under one roof, with one quality system, and one accountability chain.
- 33 years of high-volume stamping experience. VOLCRIX has been running high-volume progressive die lines in our Yueqing, Wenzhou factory since 1991. Many of our automotive Tier 1 customers have shipped with us for over 15 years.
- 40 presses under one roof. Bruderer high-speed presses for precision features, mechanical presses for structural parts. We have the capacity to scale your program from 5,000 pieces to 1,000,000 pieces per month.
- IATF 16949 certified quality system. Automotive programs run under our IATF-certified system with PPAP capability studies, control plans, and full traceability on every batch.
- In-house tool room. Die design, build, maintenance, and repair happen in our own tool room on the same campus as production. We control lead time and quality of every die.
- One roof from blanking to plated part. Stamping, in-house tool maintenance, and plating coordination happen in one factory with one accountability chain.
- 500+ active export customers. North American automotive Tier 1s, European industrial OEMs, and Asian electronics brands rely on our high-volume capacity for their serial production programs.
Frequently Asked Questions
What volume makes progressive die stamping cost-effective?
Progressive die stamping becomes cost-effective above 50,000 pieces per year. Below that threshold, soft tooling (laser cutting, 3D-printed dies) is usually cheaper because you avoid the 25,000 to 80,000 USD tooling investment. Above 100,000 pieces per year, progressive die stamping is almost always the lowest per-piece cost option.
How do you scale production from prototype to high volume?
The path runs through three gates. Gate 1 is DFM validation, where we confirm the design can be stamped at the required tolerances. Gate 2 is soft tool bridge production, where 1,000 to 5,000 pieces validate fit and function while the hard die is being built. Gate 3 is PPAP qualification, where we run capability studies and get customer sign-off before serial release. Each gate typically takes 2 to 4 weeks.
What is the maximum production capacity at VOLCRIX?
Our 40 presses can produce up to 1,000,000 pieces per month of small-to-medium stampings (under 100 mm length). For larger structural parts above 100 mm, typical monthly capacity is 100,000 to 300,000 pieces. We can flex capacity by adding shifts for programs that scale rapidly.
What is PPAP and when is it required?
PPAP (Production Part Approval Process) is the automotive industry standard for qualifying new parts and processes. PPAP is required for any part going into a vehicle program. Levels range from Level 1 (warranty only) to Level 5 (full materials and capability studies). Most VOLCRIX automotive customers request Level 3, which includes dimensional reports, material certificates, and capability studies.
How do you manage die maintenance during high-volume production?
We schedule preventive die maintenance every 50,000 to 100,000 strokes depending on material. Maintenance includes punch inspection, die polishing, stripper adjustment, and clearance check. We keep spare punches for high-volume dies so maintenance does not stop production. For critical Tier 1 programs, we maintain a backup die that can be swapped in within 24 hours.
What is your typical on-time delivery rate for high-volume programs?
For serial production, our on-time delivery rate is above 97 percent over the past two years. We use kanban release patterns and safety stock to buffer against short-term variability. For new program ramp-up, the first 3 to 6 months typically run at lower OTD as we tune capacity and process.
Do you offer vendor-managed inventory for high-volume customers?
Yes. For high-volume automotive and industrial customers, we offer VMI programs with safety stock held at our factory and released against your call-off. We typically hold 1 to 2 months of safety stock and replenish against your 12-month forecast. VMI reduces your inbound inspection cost and ensures supply continuity.
How do you handle engineering changes during high-volume production?
Engineering changes are managed through our ECN process. For die-level changes, we evaluate whether the change can be made within the existing die (die modification) or whether a new die is required (die rebuild). Modification typically takes 1 to 2 weeks; rebuild 4 to 6 weeks. We always maintain the previous revision die for a transition period to avoid supply interruption.
Certifications and Standards
VOLCRIX operates under the following certified quality and compliance systems:
- ISO 9001:2015 — Quality Management System
- IATF 16949:2016 — Automotive Quality Management
- ISO 14001:2015 — Environmental Management System
- ISO 45001:2018 — Occupational Health and Safety
- RoHS — Restriction of Hazardous Substances compliance for EU exports
- REACH — EU chemicals compliance for exported components
- CE marking support for finished assemblies where applicable
- Conflict minerals (3TG) disclosure and CFSI template on request